BICYCLE COCKPIT · FORGED SEATPOSTS
Forged aluminium seatposts, built as a two-piece assembly.
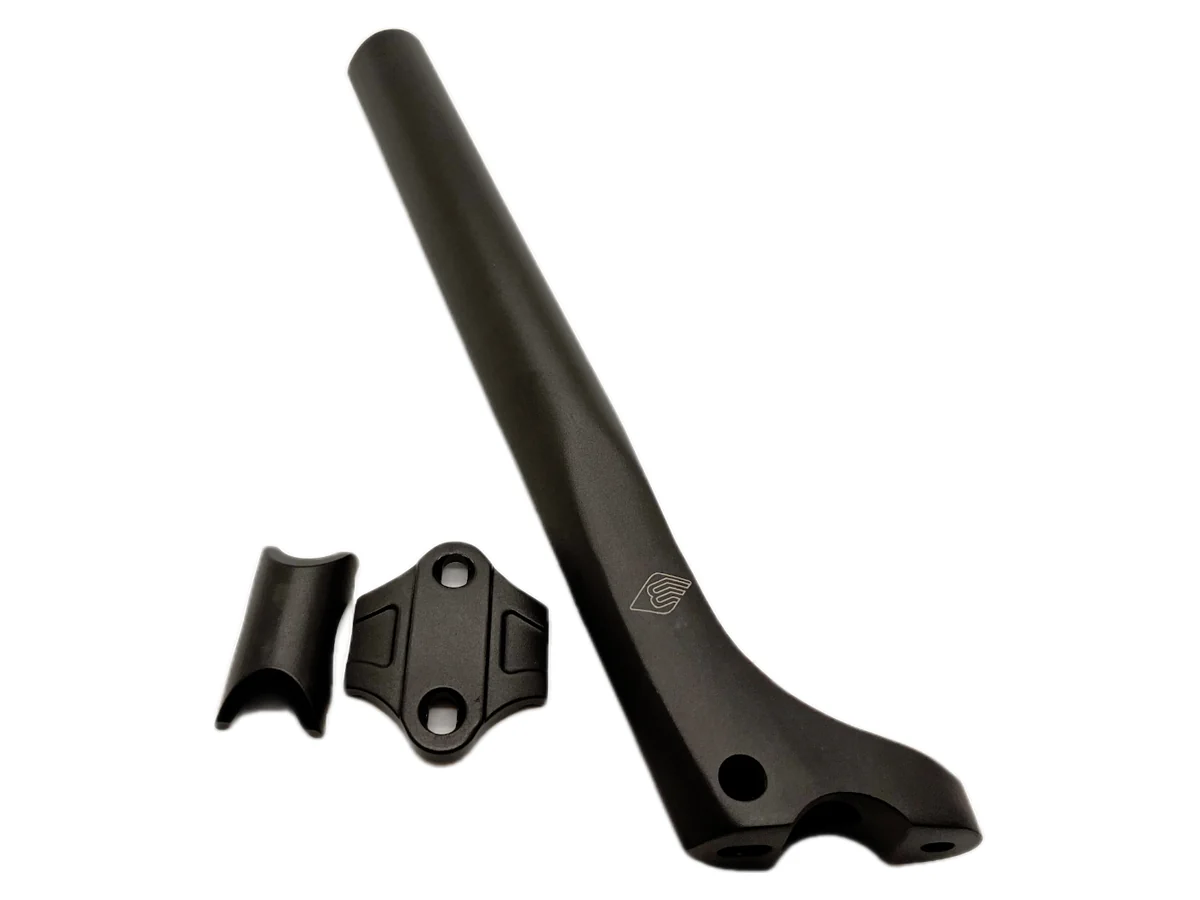
The XPF-SP is forged as two pieces — head and post — then CNC-machined at the rail clamp, insertion end and keyway. Ø28.6 interface as standard, with other diameters and lengths cut to your drawing.
WHY FORGED
A seatpost bends at the head. That is where forging earns its cost.
A seatpost carries the rider’s weight through a lever arm that peaks at the saddle clamp. Machine that head from billet and the grain runs across the bend; forge it and the grain follows the load path. Four reasons the XPF-SP is forged rather than cut:
1. Grain follows the bend
Closed-die forging turns the head’s grain along the saddle-clamp curve instead of cutting it off at the bend — the spot where fatigue cracks begin on billet-machined parts.
2. Two pieces, one datum
Head and post are machined from a shared reference, so the rail axis, clamp face and insertion end stay square to each other. That alignment is what stops saddles creeping under load.
3. Anodising has nothing to hide
Forged 6061 has no casting porosity to bloom through the anodised layer. Sand-black and sand-silver finishes stay even across the head, tube and clamp faces.
4. Material only where it works
Near-net forging leaves a controlled wall through the post and a thicker section at the head, instead of a uniform billet wall that is heavy in the wrong places.
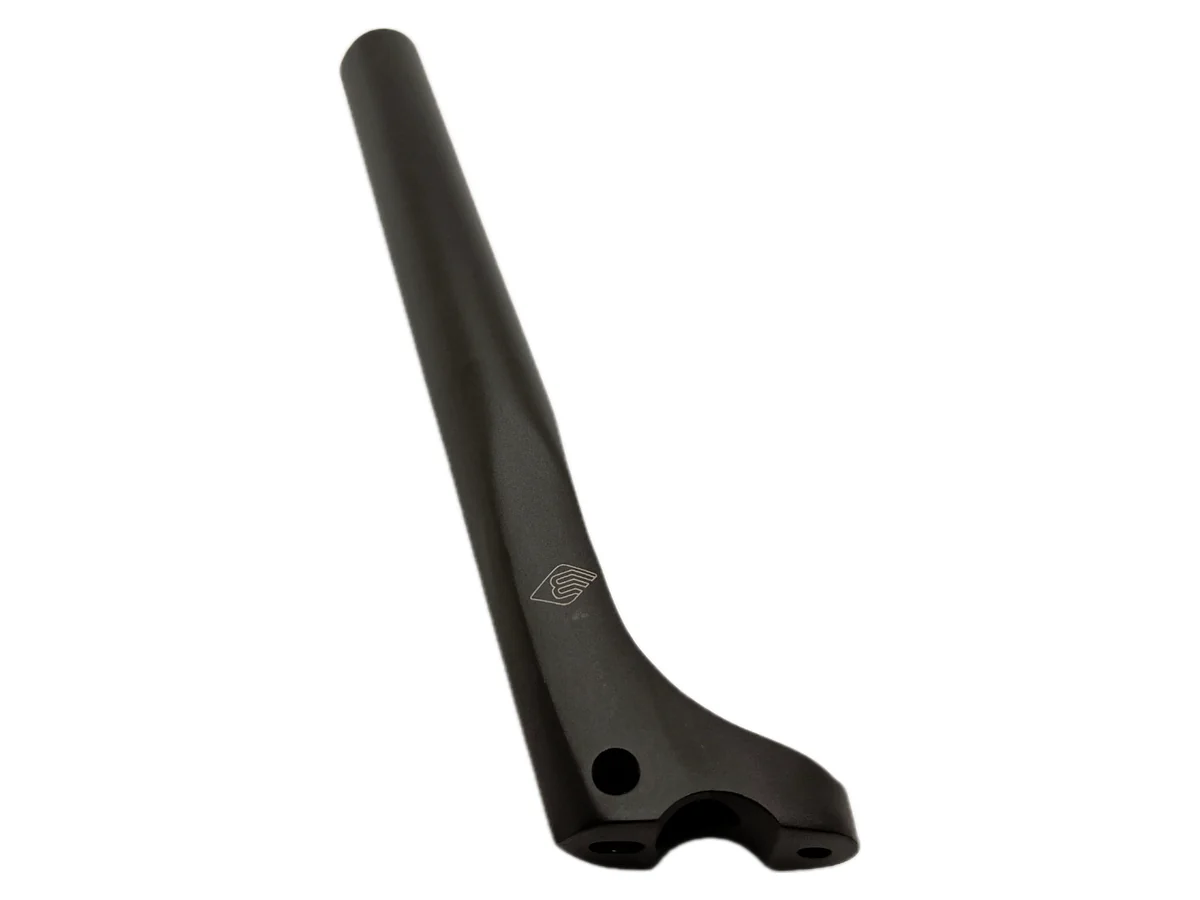
Setback head, two-bolt rail clamp and laser-marked insertion scale — forged, machined and anodised in-house.
PART FAMILIES
What we forge for cockpit and seat programs
XPF-SP complete seatpost
Setback seatpost heads
Seatpost sub-assemblies
Dropper & seat-clamp hardware
ENGINEERING
Built to the interface tolerances a cockpit needs
| Requirement | How XPF meets it |
|---|---|
| Interface | Ø28.6 standard; other insertion diameters, wall profiles and shims to drawing |
| Length & profile | Cut and machined to the length on your drawing — straight or setback |
| Head & clamp | One- or two-bolt micro-adjust rail clamps; forged or machined clamp bodies to your saddle-rail geometry |
| Material | 6061-T6 standard; 6063, 6082 and 7075 on request — mill certificate per alloy batch |
| Machining | ±0.01 mm features per drawing review: insertion end, keyway, clamp slots and thread interfaces |
| Finish | Type II / III anodising, sandblast matte, colour matching and laser marking |
| Validation | CMM dimensional report, hardness and spectrometer checks; PPAP / FAI documentation on request |
Every program is quoted from your drawing and approved specification — not from a catalogue page. If a dimension or load case is not on the drawing, we ask before quoting. The same discipline runs through our CNC machining and CNC-to-forging programs.
MATERIALS & FINISH
6061-T6 as standard, 7075 when the brief demands it
Most seatpost programs run in 6061-T6: it forges cleanly, takes a deep anodised finish and keeps cost sane. Where a program needs higher stiffness or thread strength at the clamp, we forge 7075-T6 and machine it to the same tolerances.
- 6061-T6: 310 MPa tensile, the standard choice for seatposts
- 7075-T6: 572 MPa tensile, for high-stiffness or weight-critical programs
- Finish: Type II / III anodising, sandblast matte, colour matching
- Laser marking: insertion scale, logo and part number
- Mill certificate traceable to the ingot lot with every batch
PROGRAM FIT
One supplier for cockpit and drivetrain
Seatposts rarely travel alone. The same forging line supplies the forged cranksets and adaptive-bike components that sit on the same bike — one quality system, one shipment.
Private label & wholesale
Anodised colours, laser logo and part numbering for dealer and OEM ranges — quoted per part number.
Forging vs CNC
Already machining seatpost heads from billet? The CNC-to-forging page shows the honest cost crossover.
Documentation you can audit
CMM, hardness and spectrometer records, plus PPAP / FAI on request — the full picture on Engineering & Quality.
FROM DRAWING TO SHIPMENT
How a seatpost program runs at XPF
- Drawing reviewAn engineer checks forgeability, wall sections, clamp geometry and insertion datums — feasibility opinion and cost range in 3 working days.
- Die design & cuttingTooling is designed and cut in-house, typically about 15 days — revisions never queue at an outside die maker.
- Forging & heat treatmentClosed-die forging on 300–2500T presses, then solution treatment and ageing to T6 per batch certificate.
- CNC finishingRail clamp faces, insertion end, keyway and threads machined to ±0.01 mm per drawing review in our own CNC shop.
- Finish & inspectionAnodising, laser marking, then CMM dimensional checks and material records ship with the parts.
BEFORE & AFTER
From forging blank to finished post
The blank on the right is the part before machining: closed-die forged, trimmed and heat-treated. Machining then establishes the rail clamp, insertion end and keyway — and anodising finishes it. Nothing is subcontracted between these steps, which is why a revision can be turned around in days rather than weeks.
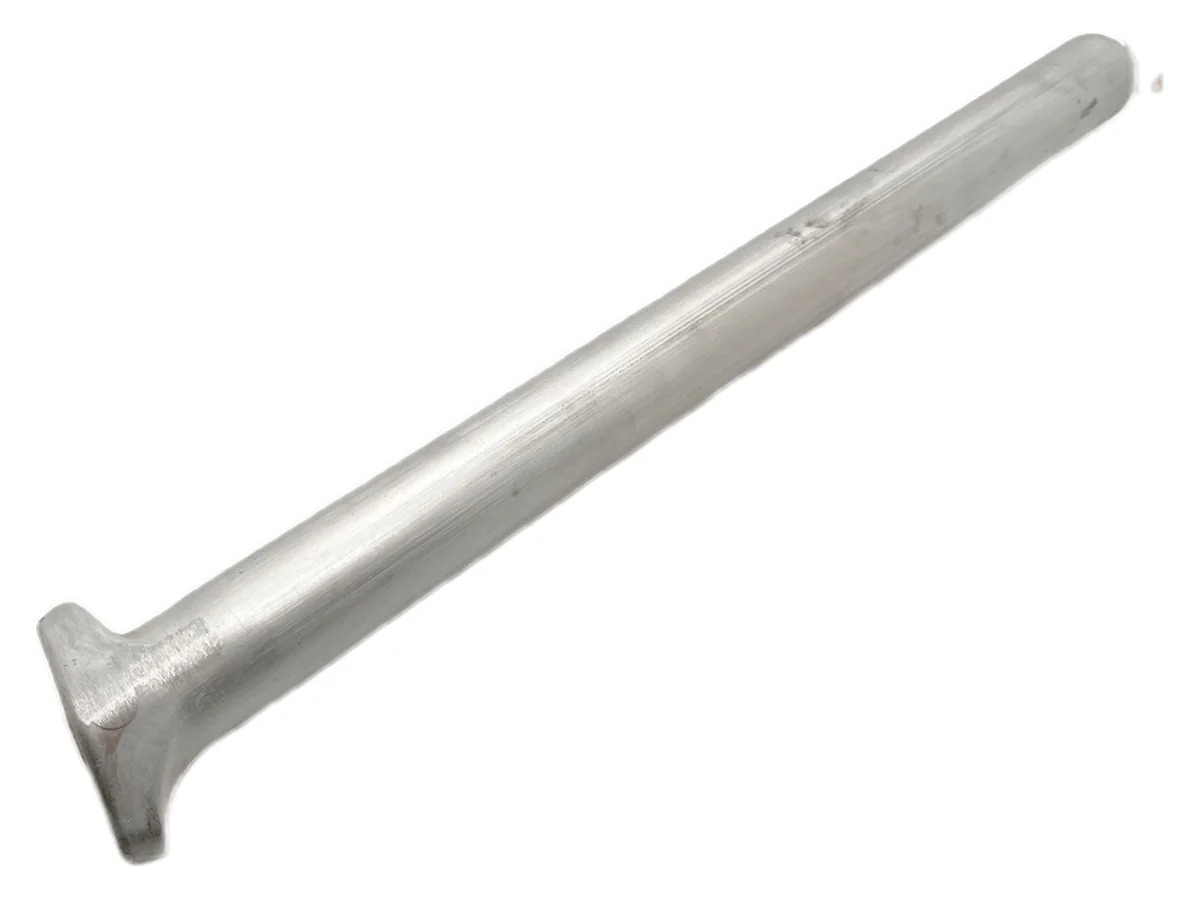
Closed-die forged seatpost blank — trimmed and heat-treated before CNC finishing.
FAQ
Seatpost questions we get from buyers
Can you produce a seatpost from our drawing?
Yes. Send STEP, DWG, DXF or PDF and an engineer reviews forgeability, wall sections and clamp geometry, then replies with a feasibility opinion and cost range in 3 working days. NDAs are standard for new cockpit designs.
What seatpost diameters can you supply?
Ø28.6 is the standard interface. Other insertion diameters, wall profiles and shim arrangements are quoted from your drawing — we do not publish a catalogue range we cannot certify.
Is the seatpost forged or machined from billet?
It is a two-piece forged assembly: the head and post are closed-die forged, then CNC-machined at the rail clamp, insertion end and keyway. That keeps grain flow through the bend while holding the interface tolerances a cockpit needs.
Which alloys do you use for seatposts?
6061-T6 is standard — it forges cleanly and anodises evenly. 6063, 6082 and 7075 are available on request. Every batch ships with a mill certificate traceable to the ingot lot.
What head and clamp options are available?
One- or two-bolt micro-adjust rail clamps, forged or machined clamp bodies, and saddle-rail geometry to your drawing. Setback offsets are machined per frame design rather than picked from a list.
Do you supply dropper seatpost parts?
We forge and machine the structural parts around a dropper post — collars, saddle-clamp heads, actuator levers and cable guides — not the hydraulic cartridge. Send the assembly drawing and we will confirm which parts fit our process.
What finishes and branding can you apply?
Type II and Type III anodising, sandblast matte, colour matching to your frame, plus laser marking for insertion scales, logos and part numbers. Colour chips are provided before production.
Do you supply private-label and wholesale programs?
Yes. We quote per part number for OEM, private-label and dealer ranges, including anodised colours, laser logo and part numbering. Batch size is based on part dimensions and die amortisation, not a factory minimum.
What quality documents come with each shipment?
A mill certificate per alloy batch and a CMM dimensional report with every shipment; hardness and spectrometer records are kept per batch, and PPAP / FAI packages are available on request.
What lead time should we plan for?
Feasibility feedback comes within 3 working days. Die design and cutting typically take about 15 days, with first samples 3–5 days after die try-out. Production is scheduled after sample approval.
Designing a seatpost around your frame?
Send one drawing — feasibility opinion and cost range from an engineer, not a salesperson.